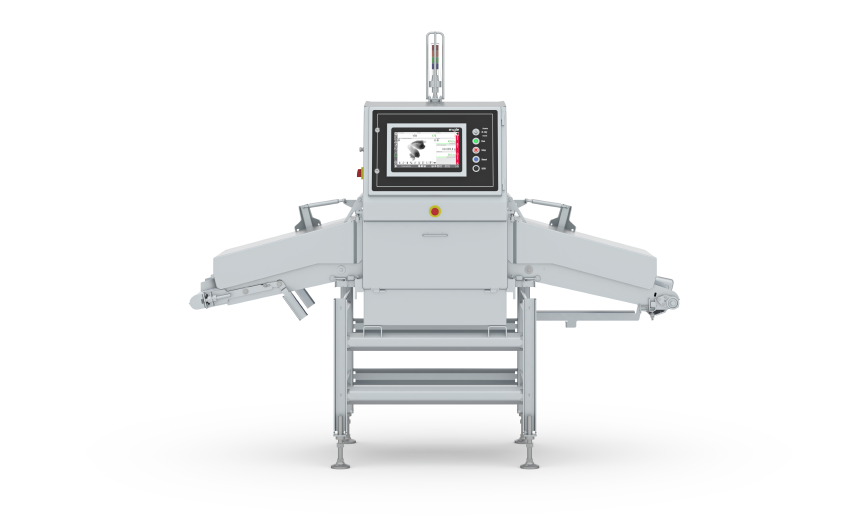
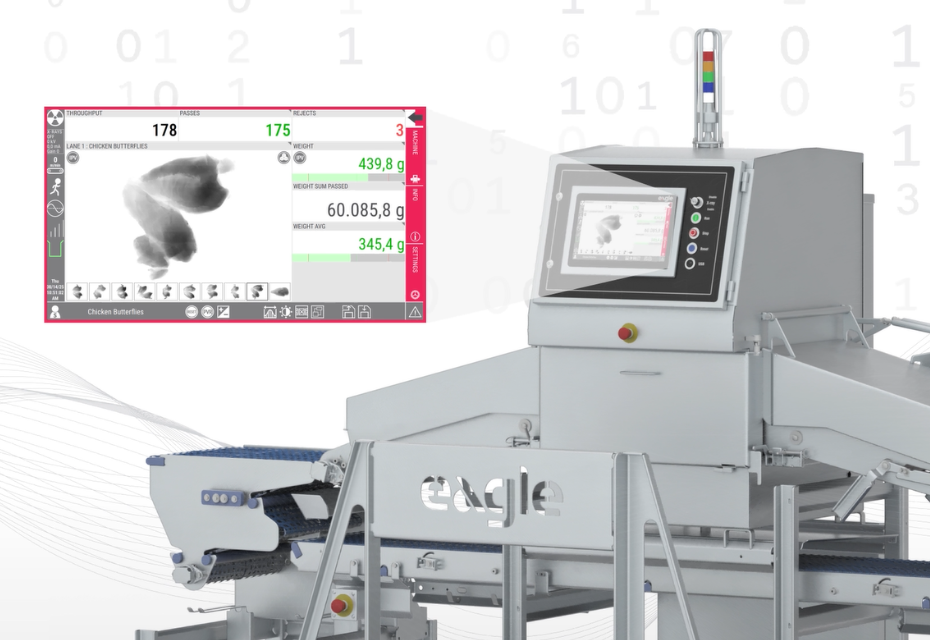
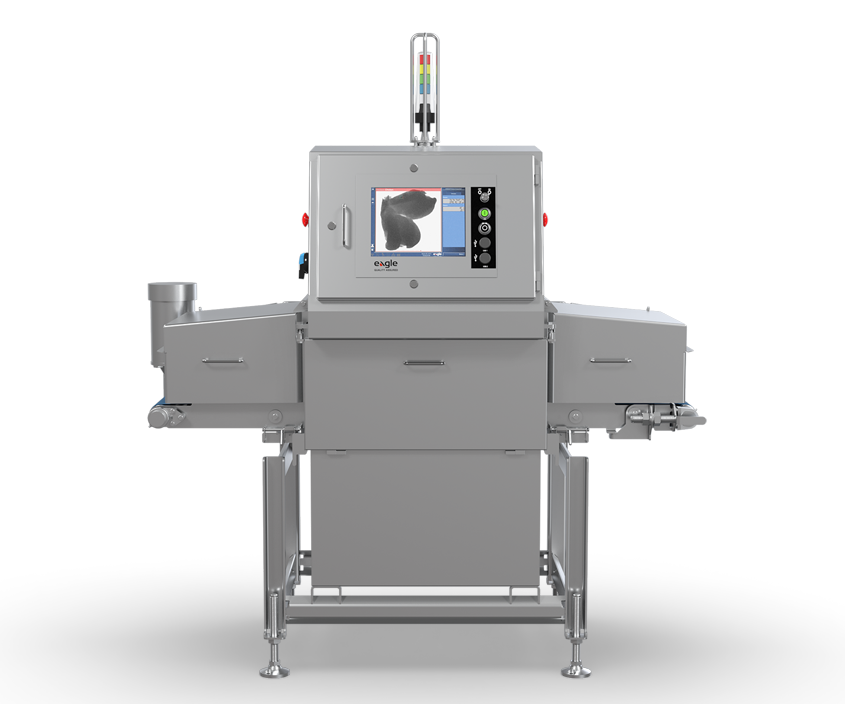
Raw Unpackaged Product RMI 400 X-ray Inspection System

Powered by SimulTask™ 6, next‑gen image intelligence, the RMI 400 delivers advanced x-ray inspection for raw unpackaged product, providing enhanced bone and contaminant detection. Designed for processors with stringent daily sanitation and hygiene requirements.

Request RMI 400 Quote
RMI 400 X-ray Inspection System

THE EVOLUTION OF INTELLIGENCE Introducing SimulTask™ 6

Experience the evolution of intelligent x-ray inspection performance.

Designed to adapt to evolving applications, line speeds, and operational requirements, SimulTask™ 6 provides a scalable software platform that delivers clear data interpretation and repeatable detection results across production environments.

SimulTask™ 6 enhances product quality and yield with:

  • Advanced sorting and classification
  • Detailed reject insights to identify root causes
  • Unnecessary waste reduction
  • Full performance visibility through live production statistics


Explore SimulTask™ 6 Capabilities

~0.1 sec

Real-time analysis

> FRR

Less false rejects

RMI 400 Machine Specifications

RMI 400

  • Primary Application

    Raw, fresh, unpackaged boneless poultry products (breasts, tenders, thighs, nuggets, or legs); seperated or bulk

  • Contamination Detection

    Metal, glass, stone, bone, high-density plastics, rubber, low-density contaminants

  • Quality/Integrity Inspection

    Bones, contaminants, mass, grading

  • Compliance/Validation/ Reporting

    User management, guided performance verification routine (PVR), machine health checks, reject bin
    monitoring, risk-assessment support

  • Lane Configuration

    Single or multi-lane system

  • Conveyor Speed

    Up to 73 m/min (240 ft/min); conveyor speed ranges are determined by the selected motor

  • Throughput

    Up to 120 products/min per lane

  • Maximum Product Height

    Up to 70 mm (2.75”)

  • Detector Technology

    0.1–0.8 mm PXT™ photon-counting detector options; 0.4 mm standard

  • X-ray Generator

    420 W, up to 84 kV, up to 5 mA, Berilyum or Glass Tube

  • Display/HMI

    15.6” PCAP touchscreen, Full-HD (1920 × 1080), 250 GB memory

  • Operating System

    Windows 11 LTSC

  • Inspection Software

    SimulTask™ 6

  • Operating Environment

    0–24°C (32–75°F), 25–90% RH non-condensing

  • Traceability/Reporting/ Connectivity

    Eagle Repository™, TraceServer™, PDF reporting, centralized storage, OPC-UA, Ethernet/IP

  • Safety Features

    Up to Category 3 / PLd (EN13849) safety circuit with HMI visibility, LOTO disconnect, compliant to 21 CFR 1020.40, 21 CFR 179.21; <1 μS/hr emissions

  • Ingress Protection/Hygienic Features

    IP69; type 304 stainless steel; surface finish less than 0.8μm/32μ-inch RA (ISO 21920-3); designed to NAMI Sanitary Guidelines, EHEDG, NSF, ISO, and CE standards where feasible

  • Power Supply

    230 VAC ±10%, single phase, 50/60 Hz, FLA 9.0A

  • Cooling

    4k/6k BTU shrouded AC (IP69)

  • Compressed Air

    Not required for base machine; rejects may require 5.5 bar (80 psi), 3/8” line; dry and filtered air supply

  • External Interface

    (8) rejects, (5) inputs, (9) outputs, and (4) PLC monitoring signals for: system processing, system calibrating, fault condition, x-rays on

  • Reject Options

    Free-standing single or dual-lane short retracting-nose reject; reject actuation confirmation available

  • Remote Service

    TeamViewer™ or customer-specific solution for remote service, diagnostics, and product set-up assistance; 24-hr support

  • Conveyor Length

    2,642 mm (104”)

  • Conveyor Height

    660–1,219 mm (26–48”); additional heights available upon request

  • Inspection Area at Belt

    389 mm (15.3”)

RMI 400 Built for Harsh Washdown Industries

RMI 400 is built to solve a wide variety of product safety and quality control issues for these industries.

Poultry

The RMI 400 helps improve detection, food safety, quality control, and process efficiency when installed at key control points on single or multilane production lines.

Seafood

Advanced PXT™ detector technology increases inspection capacity, improves product quality, and enhances operational efficiency.

Get a Custom Quote Today. Fast, Easy, and Expert-Backed!

Fill out the form and an expert will contact you within the next 48 hours.

"*" indicates required fields

Step 1 of 2

This field is for validation purposes and should be left unchanged.

Higher Detection Accuracy, Proven by Data

See how the MAXIMIZER RMI delivers measurable improvements in bone and metal detection using advanced imaging technology and data-backed performance results from real-world poultry applications.

MAXIMZER RMI 400

RMI 400 Advanced X-ray Inspection for Raw Unpackaged Product

SimulTask™ 6

Photon-Counting Dual Energy

Dynamic Duo of X-ray Inspection

TraceServer™

PRODUCT TESTING

SimulTask™ 6

Photon-Counting Dual Energy

Dynamic Duo of X-ray Inspection

TraceServer™

PRODUCT TESTING

RMI 400 X-ray Capabilities

Contaminant Detection

Advanced detection of physical contaminants for a variety of sizes, shapes, or location within a product.

Bone Detection

Find and reject harmful bone fragments in various meat, poultry, and seafood applications at high-line speeds.

Metal Detection

Reliable detection of stainless steel, ferrous, and non-ferrous metals in a broad range of applications.

Mass Measurement

Mass measurement provides an additional layer of process control and due diligence for better overall quality.

Advanced Product Sorting

Precise, configurable sorting based on weight, count, or physical values enables yield optimization.

Reject Sorting

Detailed reject classification reveals patterns earlier, helping quality teams identify root causes and reduce rework.

Robust Analytics Foundation

Inspection data is continuously captured and structured to support performance analysis, traceability, and continuous improvement.

Machine Health Monitoring

Continuous performance monitoring helps keep inspection results reliable and consistent over time.

Stop Waste Before It Starts: The Value of Early X-ray Inspection

Find out how strategically placing x-ray inspection machines before final packaging helps manufacturers reduce waste, improve operational efficiency, minimize rework, protect downstream equipment, and maximize overall product safety.

Talk to An expert

Eagle Service Support

Eagle by METTLER TOLEDO offers comprehensive service solutions for x-ray and FA systems. Keep your equipment performing at its best with Eagle’s 24/7 technical support, remote diagnostics, and preventive maintenance agreements that help reduce breakdowns and wear.

Learn more
Eagle’s
 Support Services

Industry Resources for Meat and Poultry

Poultry

RMI 400 – Features & Belt Removal

See how fast belt removal is on the RMI 400 and learn about other easy-to-use features in this machine demonstration.

Poultry
Insertion Points for Raw Chicken Inspection

Discover the key inspection points for x-ray systems in poultry processing and how they help optimize operational efficiency.

Poultry
Automated Poultry Bone Inspection with PXT™ in Action

Breakthrough poultry inspection technology, PXT™, helps processor achieve bone detection down to 1 mm.

Poultry
Choosing the Right X-ray Technology for Bone Detection in Poultry

Find out how PXT™ compares to previous poultry bone detection technologies and how x-ray systems equipped with it provide superior results.

What our Customers are saying

"Quality is number one in everything we do, it’s our focus—that and having the highest safety standards. An extra layer of food safety was required to catch items like a stone, or other foreign objects that a metal detector can’t detect.”
 Stephano CS Testimonial Tab Slider Logo
Sean Frank CEO
"We were very impressed with Eagle’s on-site service. The team adjusted the equipment to meet our needs perfectly."
 Iglo Food Group
Mr. Arno Strotmann Project Manager
"The x-ray’s software program is very intuitive. It’s simple to set up and program. I learned a great deal from Eagle’s service department on how to run the machine and appreciate their know-how, availability 24/7 and professionalism."
 Edesia Testimonial Slider Logo
Tim Pheland Process Engineer
"Quality is key for us. Now, thanks to the Eagle Bulk 415 PRO we can totally say our products are contaminant free and we truly believe this will let us keep growing and exploring new markets."
 Higos El Pajarero
Mrs. Fuensanta Carrillo Sales and Marketing Manager, Higos El Pajarero
“When first presented with the idea of inspecting our products using x-ray inspection systems, we doubted that it could help us to improve and assure the quality of their products; now it is a fundamental part inside of our system of quality.”
 Kowi
Ramiro Espinoza Kowi’s Plant Director
"Going forward, any new inspection systems or upgrades to current inspection technologies will be x-ray inspection systems, they are extremely reliable, easy to operate and easy to maintain."
 Fabric sample 2
Merrily Blasi Quality Assurance Manager
"These machines do an excellent job of looking for and pinpointing any foreign matter, with instant and easy-to-use metal detection capabilities. And they can be taught and programmed to identify other unwanted substances by measuring product density. "
 Unilever Canada
Galen Sienicki Factory Director
"The Eagle x-ray machine has resulted in a dramatic reduction of bones in our boneless products—basically down to zero. By purchasing a dual-lane system, we’re able to double our output, or run different products at the same time."
 Giannone Poultry
Bruno Giannone Vice-President and CEO
"We chose Eagle’s Pack 430 PRO because of the machine’s software capabilities - in particular, the multitask features which offered more options, compared to competitors’ machines, such as checkweighing."
 Schuman Cheese
Vincent Angiolillo VP Engineering and R&D Strategic Initiatives, Schuman Cheese, Inc.

Is X-Ray Inspection Right for Your Meat or Poultry Processing Line?

What can x-ray inspection detect in raw meat and poultry? 

X-ray inspection can detect bone fragments and physical contaminants such as metal, glass, stone, and some plastics in raw meat, poultry, and seafood. Systems such as the Eagle RMI 400 can also perform mass measurement for additional quality control. 

How small of a bone fragment can poultry x-ray inspection detect? 

Detection capability depends on the product and system configuration. With Eagle’s PXT™ photon-counting detector, the RMI 400 can detect bone fragments down to 1 mm in poultry. 

Can x-ray inspection systems withstand daily washdowns? 

Yes. X-ray systems designed for raw meat and poultry processing can be built specifically for high-sanitation environments. The RMI 400 is IP69-rated and features a curtainless design and easy-to-remove belt to support fast daily sanitation in harsh washdown environments. 

What food products can raw material x-ray systems inspect? 

Raw material x-ray inspection systems can be used for meat, poultry, and seafood processing applications. The RMI 400 is designed for medium-throughput lines with stringent hygiene requirements for poultry breasts, tenders or butterfly breasts. 


Any Questions? We Are Here for You

Contact Us

Contact Us

Request information

Ask us a question
Service Support

Service Support

Available 24 hours a day, 7 days a week.

Get in Touch
Find a representative

Find a representative

Contact your local representative

View Locations