
.svg)

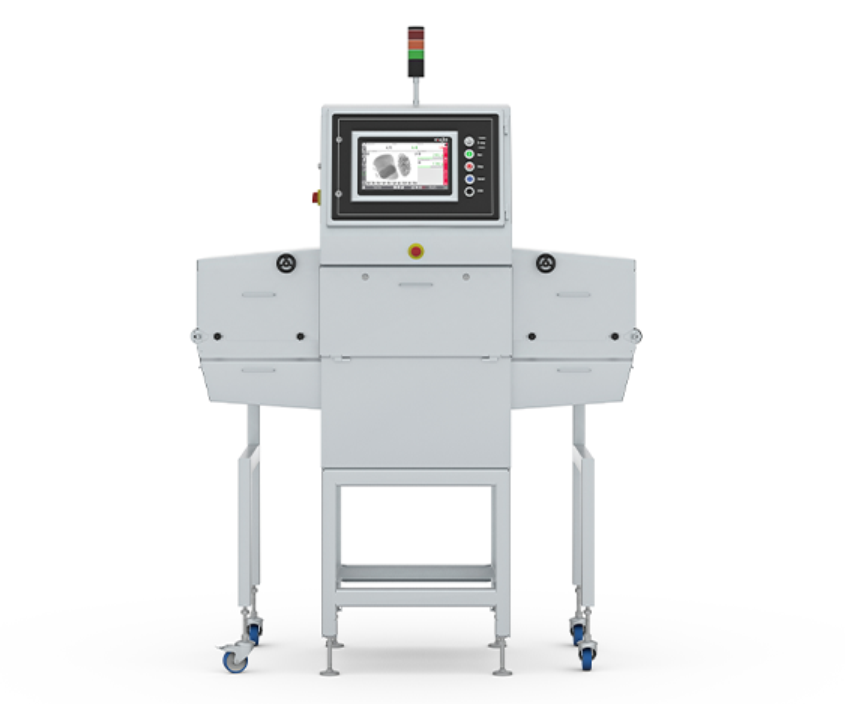
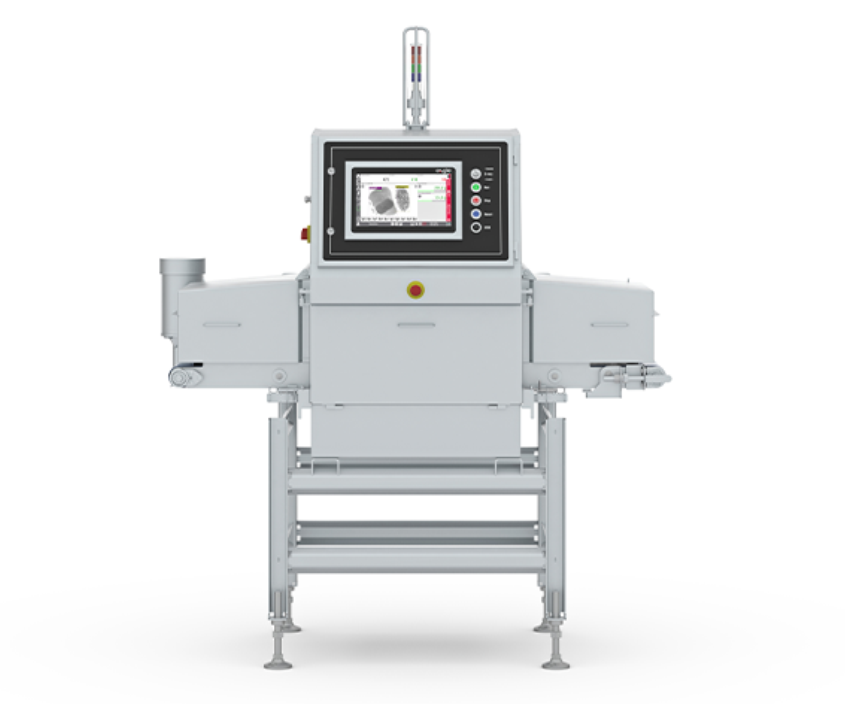
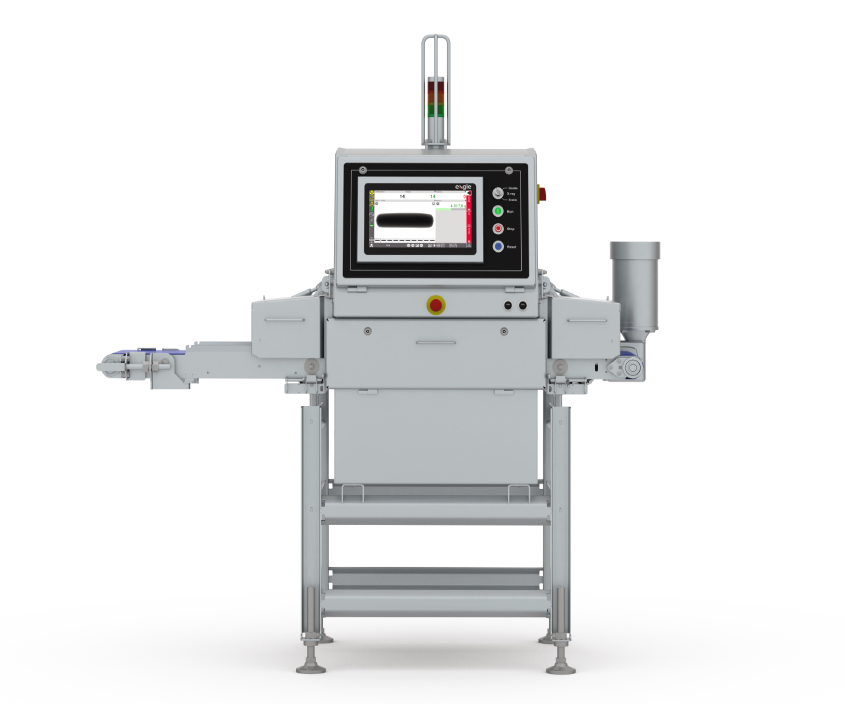
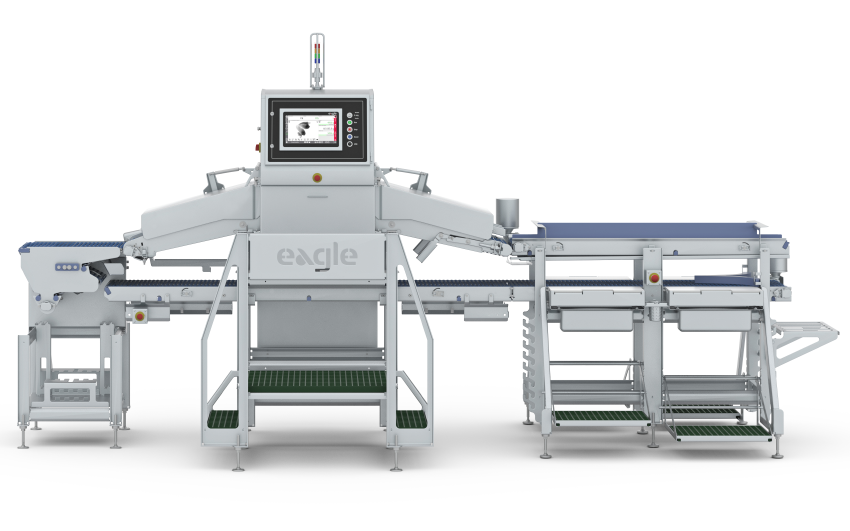
Pack 1000: X-ray Inspection of Large Packaged Product
Powered by SimulTask™ 6, next-generation image intelligence, the Pack 1000 inspects large cases and boxes of individually wrapped products, with mixed-case and multi-lane capabilities.
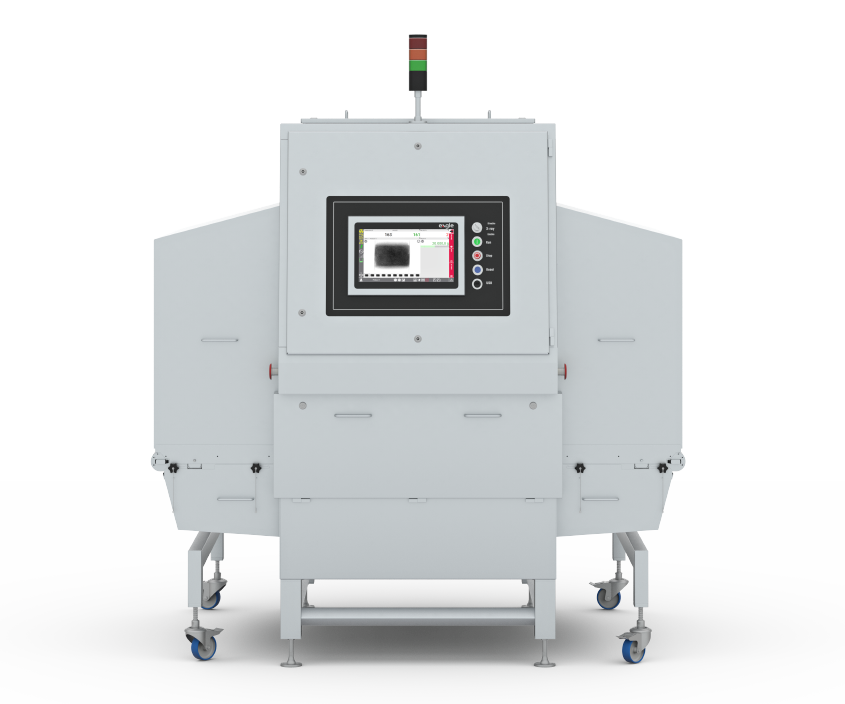

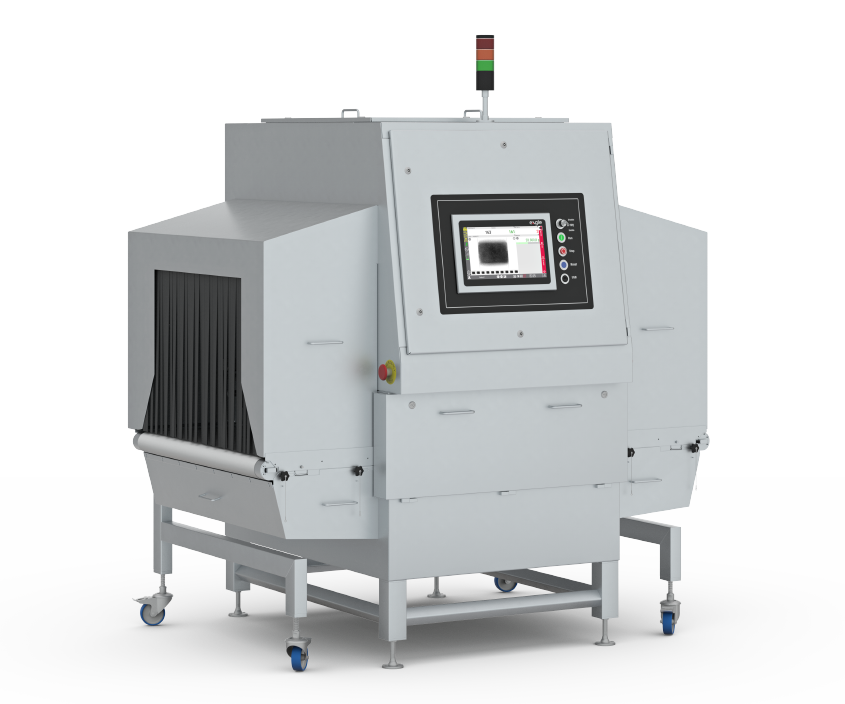


Powered by SimulTask™ 6, next-generation image intelligence, the Pack 1000 inspects large cases and boxes of individually wrapped products, with mixed-case and multi-lane capabilities.
Experience the evolution of intelligent x-ray inspection performance.
Designed to adapt to evolving applications, line speeds, and operational requirements, SimulTask™ 6 provides a scalable software platform that delivers clear data interpretation and repeatable detection results across production environments.
SimulTask™ 6 enhances product quality and yield with:

Large packaged goods in cartons, cases, sacks, bags, pouches, cups, tubs, trays, and other packaging
Metal, glass, stone, bone, high-density plastics, rubber, low-density contaminants
Missing item, clip, count, void, broken-item, mass, sorting, shape, package integrity
User management, guided performance verification routine (PVR), machine health checks, reject bin
monitoring, risk-assessment support
Single or multi-lane system
Up to 76 m/min (250 ft/min); conveyor speed ranges are determined by the selected motor
Up to 1000 products/min
Up to 609 mm (24”); see beam geometry limits
1.2 mm MDX dual energy
HR7, up to 140 kV, up to 1 mA glass tube; HR9N, up to 140 kV, up to 3 mA glass tube
15.6” PCAP touchscreen, Full-HD (1920 × 1080); 250 GB memory
Windows 11 LTSC
SimulTask™ 6
Eagle Repository™, TraceServer™, PDF reporting, centralized storage, OPC-UA, Ethernet/IP
Up to Category 3 / PLd (EN13849) safety circuit with HMI visibility, LOTO disconnect, compliant to 21 CFR 1020.40, 21 CFR 179.21; <1 μS/hr emissions
IP65 or IP69; type 304 stainless steel
0–40°C (32–104°F); 25–90% RH non-condensing
230 VAC ±10%, single phase, 50/60 Hz, FLA 9.0A
8k BTU waterless AC (IP65); 8k BTU shrouded AC (IP69)
Not required for base machine; rejects may require 5.5 bar (80 psi), 3/8” line; dry and filtered air supply
(8) rejects, (5) inputs, (9) outputs, and (4) PLC monitoring signals for: system processing, system calibrating, fault condition, x-rays on
24 VDC signal, side push arm; other rejects and reject verification sensors available upon request
TeamViewer™ or customer-specific solution for remote service, diagnostics, and product set-up assistance; 24-hr support
1,981 mm (78”)
762–1,219 mm (30–48”); additional heights upon request
1,018 mm (40”)


From raw chicken breasts or tenderloins to turkey legs and thighs, Eagle x-ray machines can be installed at many different critical control points (CCPs) on your plants production line, for enhanced poultry bone detection, safety, strengthened quality control, and improved processes for either single or multi-lane processing lines.

The seafood processing industry faces unique challenges that require specialized inspection solutions. Equipped with PXT™, the latest photon-counting x-ray detector technology, our machines offer exceptional detection capabilities for a variety of seafood products–whether frozen filets, canned goods, or bulk shelled items.

Not only do our advanced inspection technologies detect foreign objects, but they also go the extra mile by identifying voids in cheese blocks and fill level in yogurt cups. Count on our technology to maintain product safety, precise portion control, along with weight checks and package integrity for every item.

Tackling the hurdles faced by fruit and vegetable manufacturers, our Eagle x-ray systems adeptly locate foreign body contaminants that can occur from harvest to processing. Our dual energy technology is particularly effective in detecting unwanted materials in dense products like dried fruits.

From packaged foods to complex applications, Eagle’s x-ray inspection systems combine high-speed performance and advanced contaminant detection to help manufacturers protect product quality, food safety, and compliance.
Get a Custom Quote Today.
Find out if the Pack 1000 is a fit for your line, fill out the form and a team member will contact you within the next 48 hours.
"*" indicates required fields
Accurate inspection data helps food and packaging manufacturers protect product quality, support compliance, and improve production efficiency. Next-generation x-ray image processing, SimulTask™ 6 transforms inspection images into real-time insights that help teams detect contaminants, verify product quality, reduce downtime, and respond quickly to production changes.

Eagle’s Material Discrimination X-ray (MDX) technology allows food processors to differentiate organic and inorganic materials, offering superior contaminant detection for meat inspection, including foreign bodies missed by conventional methods.

Eagle’s TraceServer™ x-ray software centralizes production data and machine status from up to 32 x-ray machines into one database. It records inspection processes to help meet quality standards and is scalable to fit your company’s needs, simplifying product traceability.
Send us your product for a free test, and you’ll receive a detailed report with machine configuration, inspection data, and the Probability of Detection (POD) as a percentage, reflecting real production conditions.
The Pack 1000 improves production performance with advanced contaminant detection and quality inspection, including verification of package integrity, mass, fill level, and component counts in large packages.
Advanced detection of physical contaminants for a variety of sizes, shapes, or location within a product.
Find and reject harmful bone fragments, 2 mm or less, in various meat, poultry, and seafood applications.
Quickly and reliably verifiy package integrity, mass, fill level, and component count inside sealed packaging to enhance product quality.
Precise, configurable sorting based on weight, count, or physical values enables yield optimization.
Detailed reject classification reveals patterns earlier, helping quality teams identify root causes and reduce rework.
Inspection data is continuously captured and structured to support performance analysis, traceability, and continuous improvement.
Continuous performance monitoring helps keep inspection results reliable and consistent over time.
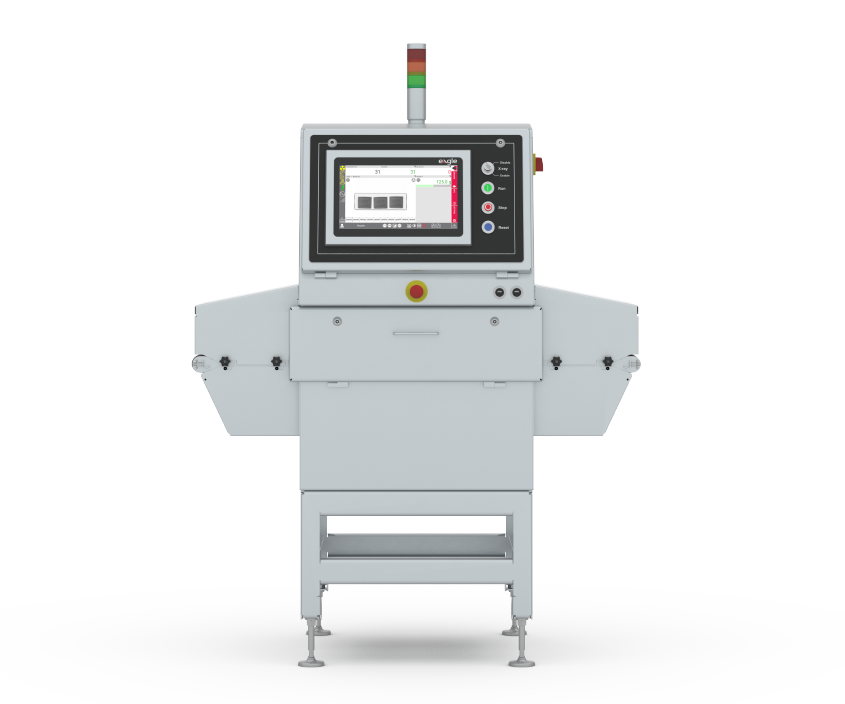

Eagle by METTLER TOLEDO offers comprehensive service solutions for x-ray and FA systems. Keep your equipment performing at its best with Eagle’s 24/7 technical support, remote diagnostics, and preventive maintenance agreements that help reduce breakdowns and wear.
Learn the key differences between HACCP and Food Safety Plans, from scope and documentation to preventive controls.
Eagle’s Pack 720 PRO with MDX technology tackles contaminant detection and offers 3 key benefits to bulk potato distributors.
Chip manufacturers can meet quality control standards for contaminant detection and weight specification with x-ray inspection equipment


What Our Customers Say