
.svg)

Pack 550 X-ray System for Large Packaged Product
Powered by SimulTask™ 6, next-generation image intelligence, the Pack 550 delivers delivers advanced contaminant detection and quality measurements for medium to large packages or containers.
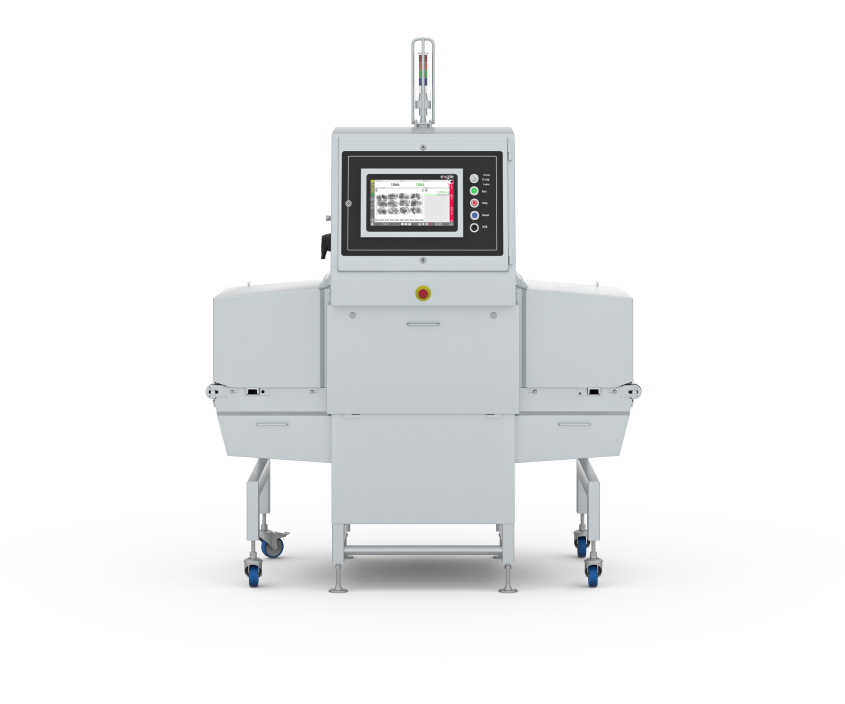


Powered by SimulTask™ 6, next-generation image intelligence, the Pack 550 delivers delivers advanced contaminant detection and quality measurements for medium to large packages or containers.
Experience the evolution of intelligent x-ray inspection performance.
Designed to adapt to evolving applications, line speeds, and operational requirements, SimulTask™ 6 provides a scalable software platform that delivers clear data interpretation and repeatable detection results across production environments.
SimulTask™ 6 enhances product quality and yield with:

Medium and large packaged goods in cartons, cases, sacks, bags, pouches, cups, tubs, trays, and other packaging
Metal, glass, stone, bone, high-density plastics, rubber, low-density contaminants
Missing item, clip, count, void, broken-item, mass, sorting, shape, package integrity
User management, guided performance verification routine (PVR), machine health checks, reject bin
monitoring, risk-assessment support
Single or multi-lane system
Up to 80 m/min (262 ft/min); conveyor speed ranges are determined by the selected motor
Up to 1000 products/min
Up to 279 mm (11”); see beam geometry limits
0.1–0.8 mm PXT™ photon-counting detector options; 0.4 mm standard or 0.4 mm single-energy
420 W, up to 84 kV, up to 5 mA, beryllium or glass tube; HR7, up to 140 kV, up to 1 mA glass tube; HR9N, up to 140 kV, up to 3 mA glass tube
15.6” PCAP touchscreen, Full-HD (1920 × 1080); 250 GB memory
Windows 11 LTSC
SimulTask™ 6
Eagle Repository™, TraceServer™, PDF reporting, centralized storage, OPC-UA, Ethernet/IP
Up to Category 3 / PLd (EN13849) safety circuit with HMI visibility, LOTO disconnect, compliant to 21 CFR 1020.40, 21 CFR 179.21; <1 μS/hr emissions
IP69; type 304 stainless steel; surface finish less than 0.8μm/32μ-inch RA (ISO 21920-3); designed to NAMI Sanitary Guidelines, EHEDG, NSF, ISO, and CE standards where feasible
0–40°C (32–104°F); 25–90% RH non-condensing
230 VAC ±10%, single phase, 50/60 Hz, FLA 9.0A
4k/6k BTU shrouded AC (IP69)
Not required for base machine; rejects may require 5.5 bar (80 psi), 3/8” line; dry and filtered air supply
(8) rejects, (5) inputs, (9) outputs, and (4) PLC monitoring signals for: system processing, system calibrating, fault condition, x-rays on
24 VDC signal, air blast, side push arm; other reject options available
TeamViewer™ or customer-specific solution for remote service, diagnostics, and product set-up assistance; 24-hr support
1,828 mm (72”), 2,438 mm (96”), 2,895 mm (114”)
762–1,397 mm (30–55”); additional heights upon request
540 mm (21.2”)


From raw chicken breasts or tenderloins to turkey legs and thighs, Eagle x-ray machines can be installed at many different critical control points (CCPs) on your plants production line, for enhanced poultry bone detection, safety, strengthened quality control, and improved processes for either single or multi-lane processing lines.

The seafood processing industry faces unique challenges that require specialized inspection solutions. Equipped with PXT™, the latest photon-counting x-ray detector technology, our machines offer exceptional detection capabilities for a variety of seafood products–whether frozen filets, canned goods, or bulk shelled items.

Not only do our advanced inspection technologies detect foreign objects, but they also go the extra mile by identifying voids in cheese blocks and fill level in yogurt cups. Count on our technology to maintain product safety, precise portion control, along with weight checks and package integrity for every item.

Tackling the hurdles faced by fruit and vegetable manufacturers, our Eagle x-ray systems adeptly locate foreign body contaminants that can occur from harvest to processing. Our dual energy technology is particularly effective in detecting unwanted materials in dense products like dried fruits.

From packaged foods to complex applications, Eagle’s x-ray inspection systems combine high-speed performance and advanced contaminant detection to help manufacturers protect product quality, food safety, and compliance.
Get a Custom Quote Today.
Find out if the Pack 550 is a fit for your line, fill out the form and a team member will contact you within the next 48 hours.
"*" indicates required fields
Accurate inspection data helps food and packaging manufacturers protect product quality, support compliance, and improve production efficiency. Next-generation x-ray image processing, SimulTask™ 6 transforms inspection images into real-time insights that help teams detect contaminants, verify product quality, reduce downtime, and respond quickly to production changes.

PXT™ photon-counting x-ray technology is an advanced dual energy detector that delivers high-resolution images and detailed product data, improving detection accuracy in complex products and reducing false rejects.

PXT™ photon-counting x-ray technology, combined with SimulTask™ image analysis software, delivers high-resolution images and real-time analysis in just one-tenth of a second, setting a new standard in detecting bones, metal, and other contaminants.

Eagle’s TraceServer™ x-ray software centralizes production data and machine status from up to 32 x-ray machines into one database. It records inspection processes to help meet quality standards and is scalable to fit your company’s needs, simplifying product traceability.
Send us your product for a free test, and you’ll receive a detailed report with machine configuration, inspection data, and the Probability of Detection (POD) as a percentage, reflecting real production conditions.
The Pack 550 helps improve production performance with advanced contaminant detection and quality inspection, including verification of package integrity, mass, fill level, and component counts.
Advanced detection of physical contaminants for a variety of sizes, shapes, or location within a product.
Find and reject harmful bone fragments, 2 mm or less, in various meat, poultry, and seafood applications.
Quickly and reliably verifiy package integrity, mass, fill level, and component count inside sealed packaging to enhance product quality.
Precise, configurable sorting based on weight, count, or physical values enables yield optimization.
Detailed reject classification reveals patterns earlier, helping quality teams identify root causes and reduce rework.
Inspection data is continuously captured and structured to support performance analysis, traceability, and continuous improvement.
Continuous performance monitoring helps keep inspection results reliable and consistent over time.
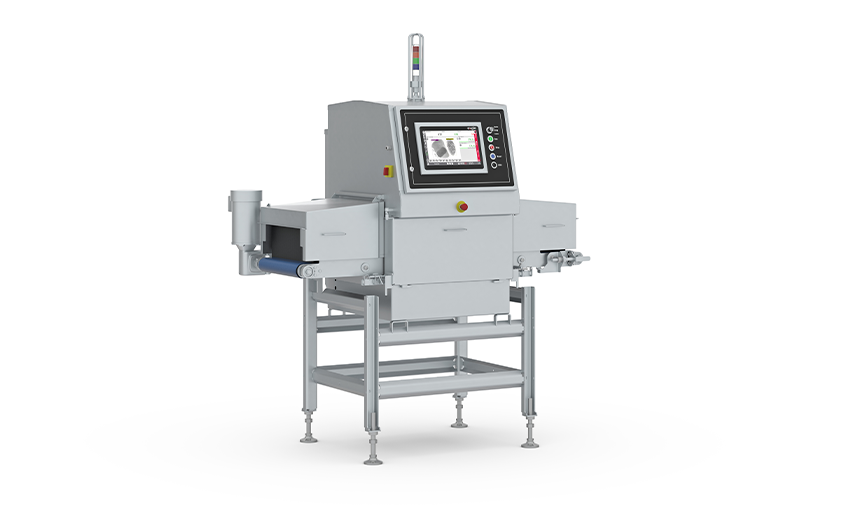


Eagle by METTLER TOLEDO offers comprehensive service solutions for x-ray and FA systems. Keep your equipment performing at its best with Eagle’s 24/7 technical support, remote diagnostics, and preventive maintenance agreements that help reduce breakdowns and wear.
Get the 4 benefits of X-ray machines for food inspection! Learn how this technology improves food safety and reduces costs for processors.
Learn how x-ray supports safety audits with easy retrieval reports, time-stamped imaging, and more!
Ensure contaminant detection, product fill level, mass measurement, package integrity, component count and more with x-ray inspection technology.
Chip manufacturers can meet quality control standards for contaminant detection and weight specification with x-ray inspection equipment


What Our Customers Say